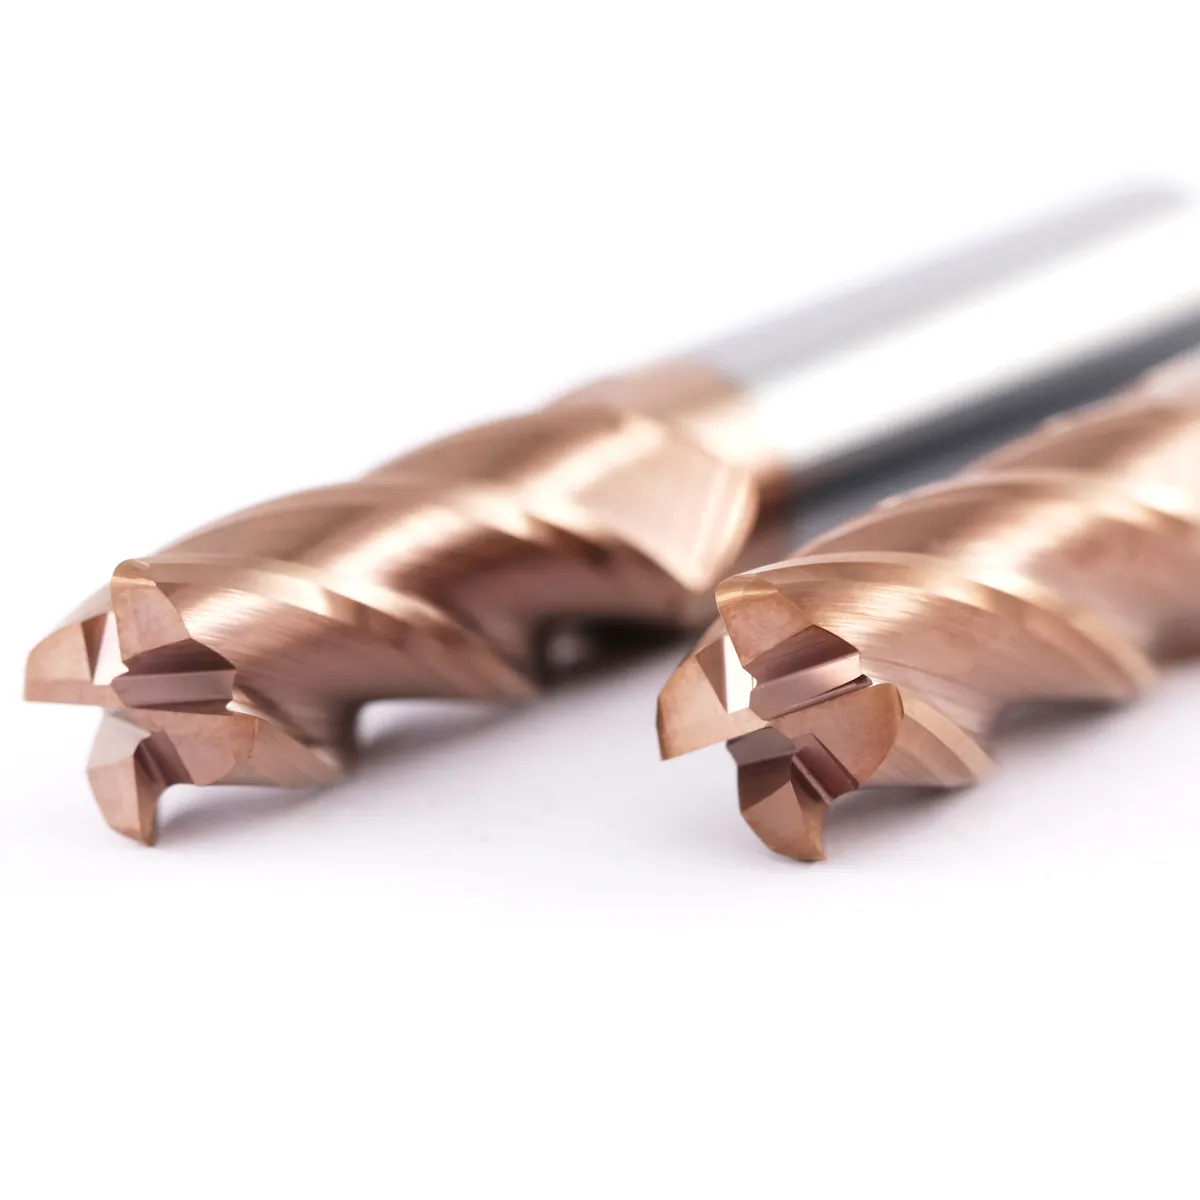
Standard Solid Carbide End Mills
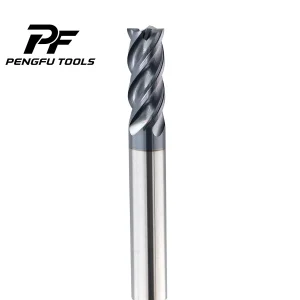
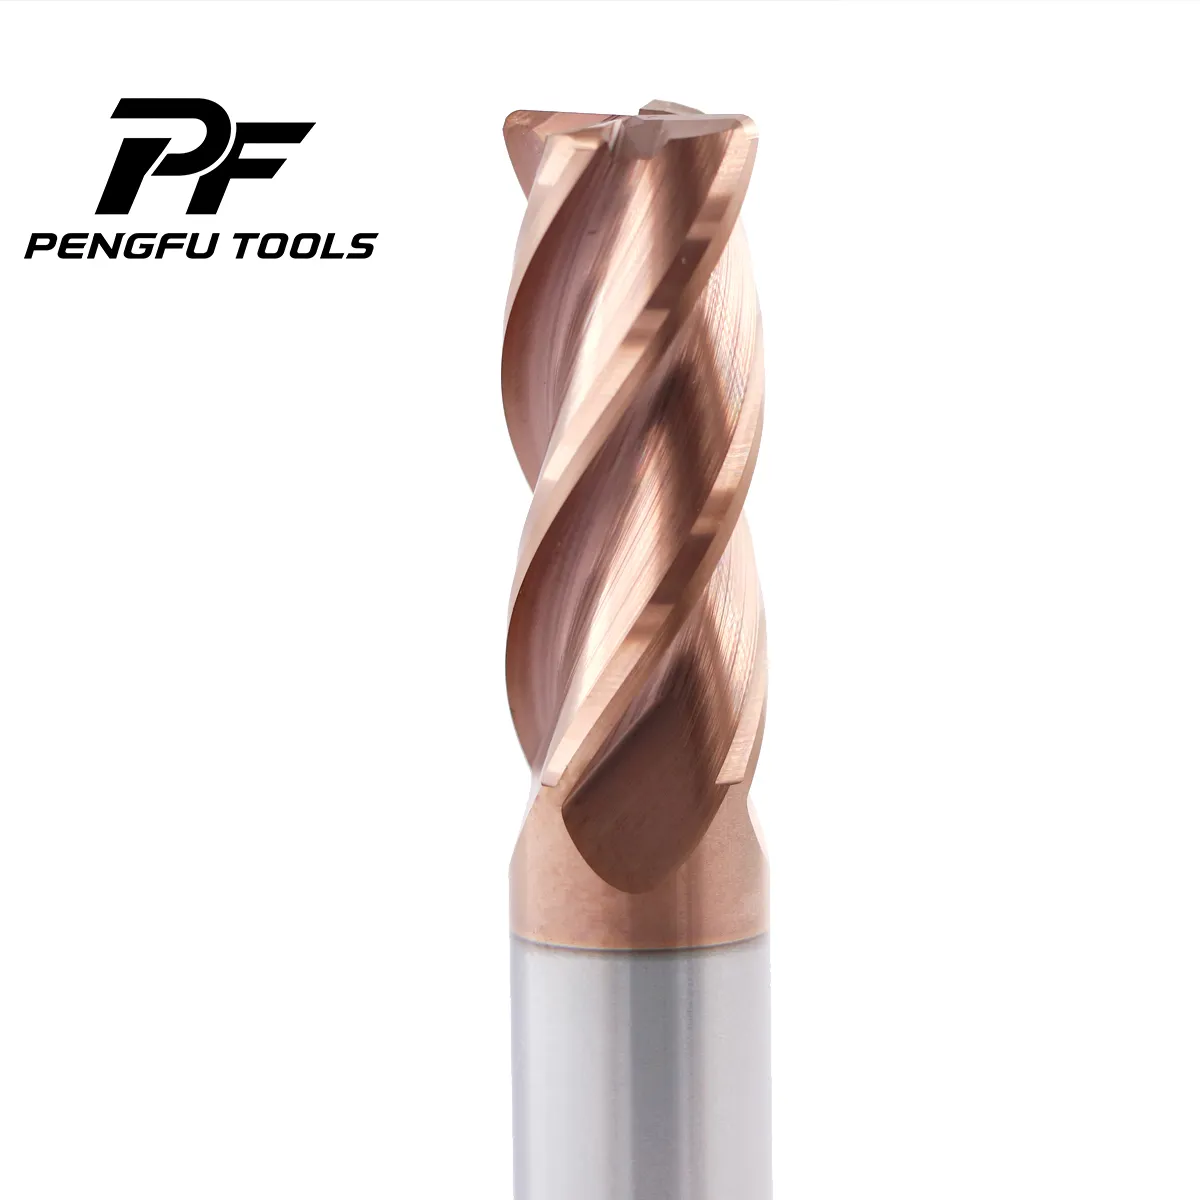
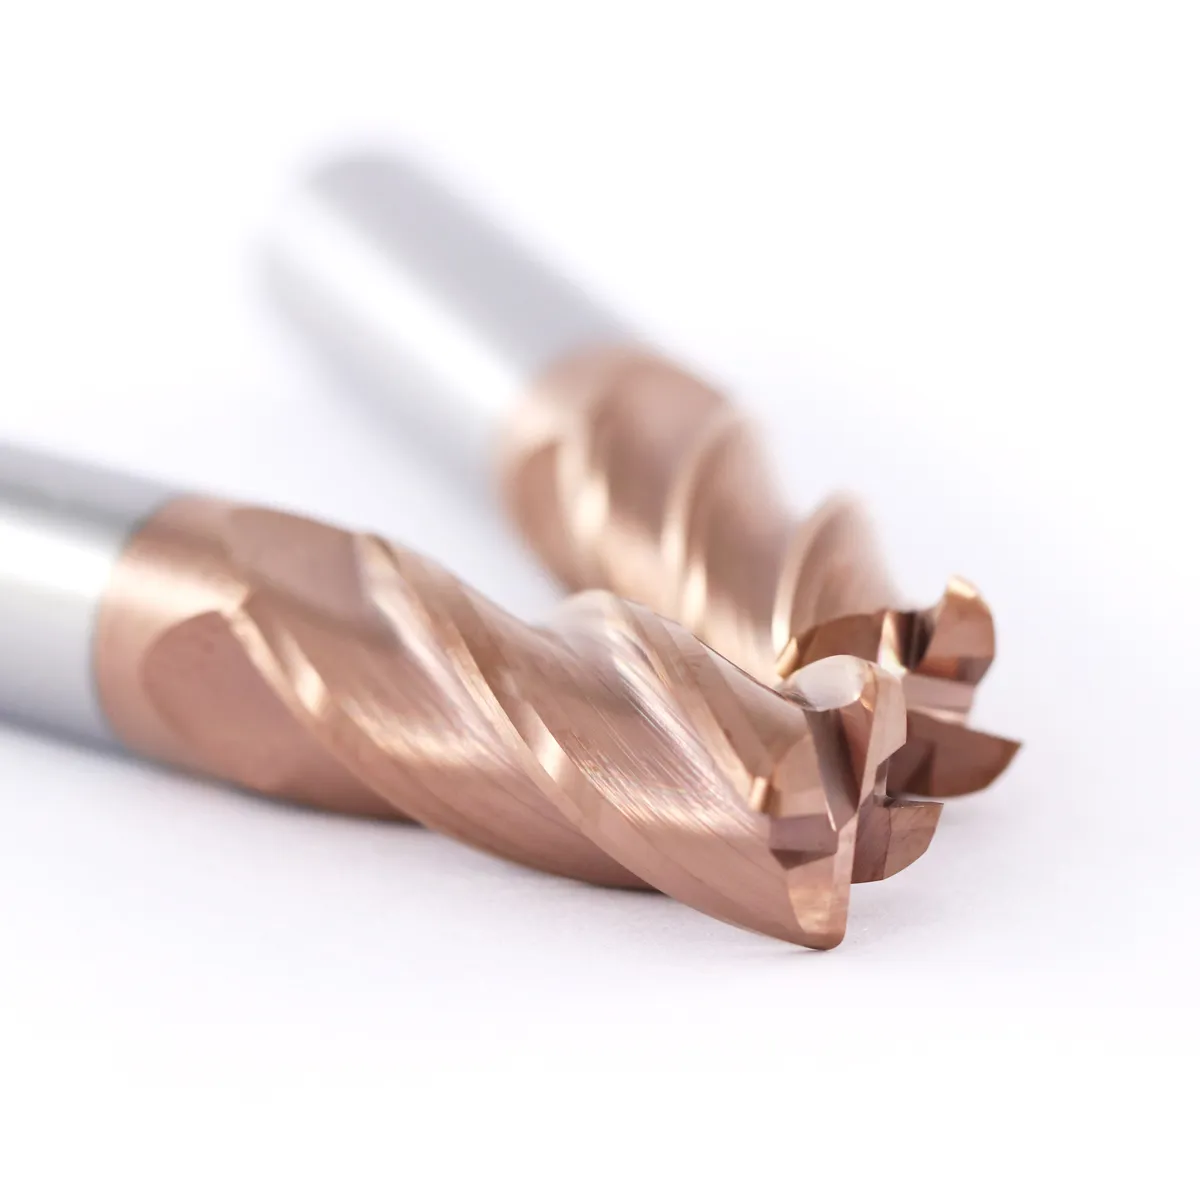
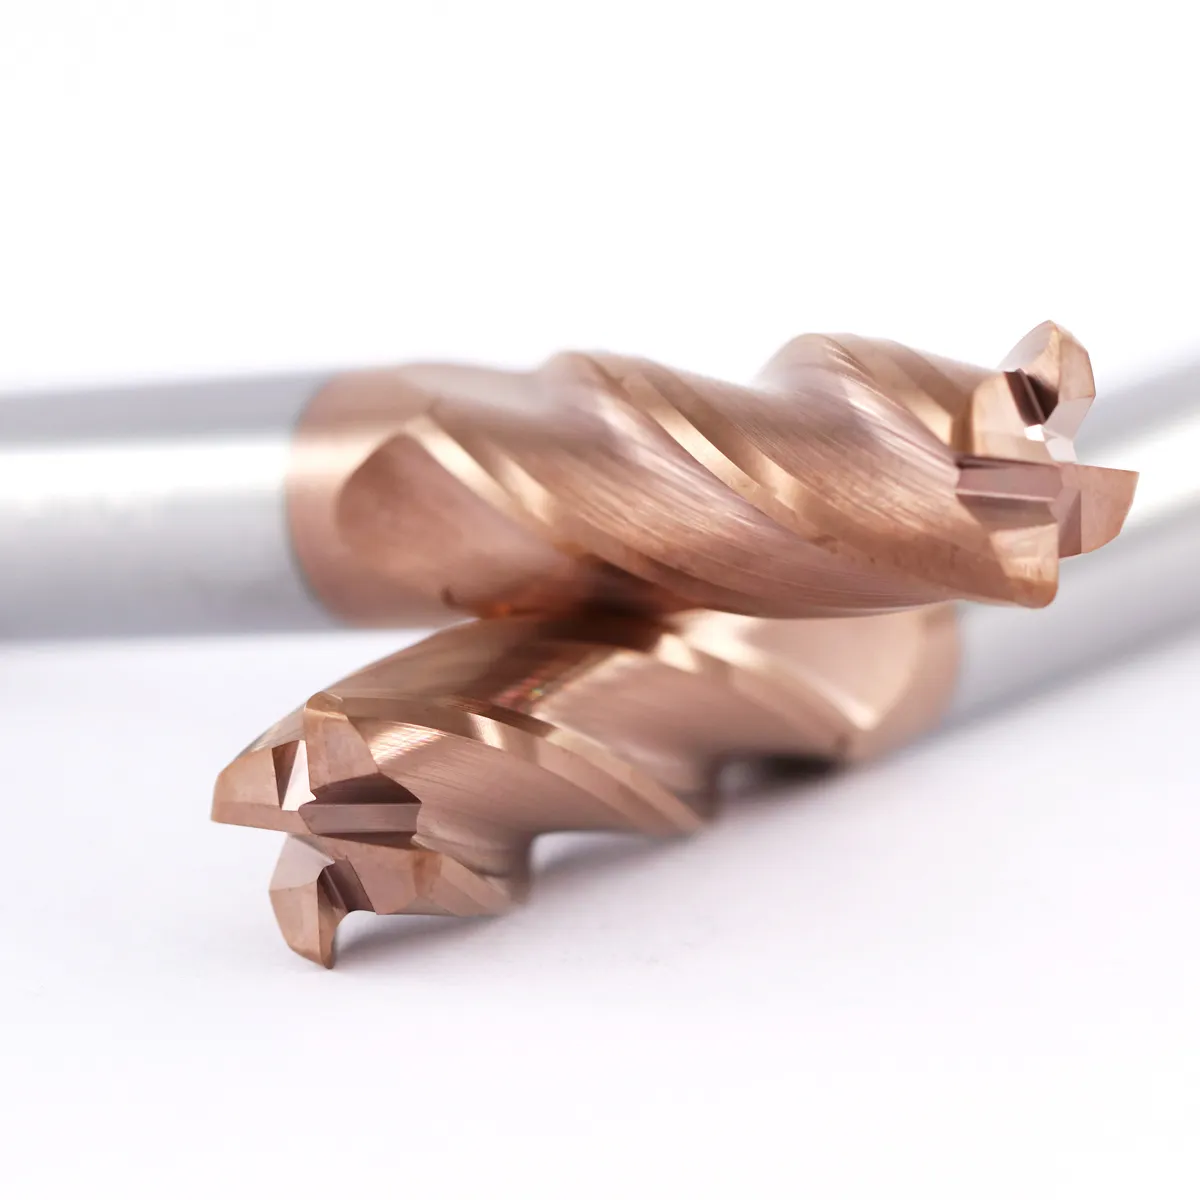
HRC55 Corner Radius End Mill 4F
Reinforced corner-radius geometry improves cutting-edge strength and stability in demanding machining.
Product Advantages
01Reinforced cutting corners
02Reduced edge chipping
03Stable profiling performance
04Consistent tool life
Technical Information
| Item | Specification |
|---|---|
| Tool Material | Premium micro-grain solid carbide |
| Geometry | 4-flute corner-radius geometry |
| Coating | Application-specific high-performance coating |
| Recommended Materials | Carbon steel, alloy steel, tool steel and mold steel with workpiece hardness up to HRC55 |
| Typical Operations | Profiling, shoulder milling, contouring, semi-finishing and finishing |
Published Specifications & Cutting Data
The following values are based on the specifications currently published for this product. Please confirm stock dimensions and machining conditions before ordering.
Product Information
| Item | Description |
|---|---|
| Product Name | TiSiN Coated 4-Flute Corner Radius End Mill |
| Tool Material | Fine-Grain Solid Carbide |
| Number of Flutes | 4 Flutes |
| End Style | Corner Radius / Bull Nose |
| Coating | TiSiN |
| Helix Angle | Approximately 30°–35° |
| Shank Type | Straight Shank |
| Cutting Direction | Right-Hand Cutting |
| Recommended Hardness | Workpiece hardness up to approximately HRC55 |
| Manufacturing Method | Precision Ground |
Reference Specifications
| Cutter Dia. D | Corner Radius R | Cutting Length L | Shank Dia. D2 | Overall Length L2 | Flutes |
|---|---|---|---|---|---|
| 1.0 | 0.2 | 3 | 4 | 50 | 4 |
| 1.5 | 0.2 | 5 | 4 | 50 | 4 |
| 2.0 | 0.2 | 6 | 4 | 50 | 4 |
| 2.0 | 0.5 | 6 | 4 | 50 | 4 |
| 2.5 | 0.2 | 8 | 4 | 50 | 4 |
| 2.5 | 0.5 | 8 | 4 | 50 | 4 |
| 3.0 | 0.2 | 9 | 3 | 50 | 4 |
| 3.0 | 0.5 | 9 | 3 | 50 | 4 |
| 3.0 | 0.2 | 9 | 4 | 50 | 4 |
| 3.0 | 0.5 | 9 | 4 | 50 | 4 |
| 4.0 | 0.2 | 12 | 4 | 50 | 4 |
| 4.0 | 0.5 | 12 | 4 | 50 | 4 |
| 4.0 | 1.0 | 12 | 4 | 50 | 4 |
| 5.0 | 0.5 | 13 | 5 | 50 | 4 |
| 5.0 | 1.0 | 13 | 5 | 50 | 4 |
| 6.0 | 0.5 | 15 | 6 | 50 | 4 |
| 6.0 | 1.0 | 15 | 6 | 50 | 4 |
| 6.0 | 1.5 | 15 | 6 | 50 | 4 |
| 8.0 | 0.5 | 20 | 8 | 60 | 4 |
| 8.0 | 1.0 | 20 | 8 | 60 | 4 |
| 8.0 | 1.5 | 20 | 8 | 60 | 4 |
| 8.0 | 2.0 | 20 | 8 | 60 | 4 |
| 10.0 | 0.5 | 25 | 10 | 75 | 4 |
| 10.0 | 1.0 | 25 | 10 | 75 | 4 |
| 10.0 | 2.0 | 25 | 10 | 75 | 4 |
| 10.0 | 3.0 | 25 | 10 | 75 | 4 |
| 12.0 | 0.5 | 30 | 12 | 75 | 4 |
| 12.0 | 1.0 | 30 | 12 | 75 | 4 |
| 12.0 | 2.0 | 30 | 12 | 75 | 4 |
| 12.0 | 3.0 | 30 | 12 | 75 | 4 |
| 14.0 | 1.0 | 45 | 14 | 100 | 4 |
| 14.0 | 2.0 | 45 | 14 | 100 | 4 |
| 16.0 | 1.0 | 45 | 16 | 100 | 4 |
| 16.0 | 2.0 | 45 | 16 | 100 | 4 |
| 20.0 | 1.0 | 45 | 20 | 100 | 4 |
| 20.0 | 2.0 | 45 | 20 | 100 | 4 |
Reference Dimensional Tolerance
| Item | Reference Tolerance |
|---|---|
| Cutter diameter D ≤ 12 mm | 0 / −0.015 mm |
| Cutter diameter D > 12 mm | 0 / −0.020 mm |
| Corner radius R | Confirm according to size and accuracy requirements |
| Shank diameter D2 | h6 available upon request |
Reference Cutting Conditions
| Workpiece Material | Material Condition | Recommended Vc |
|---|---|---|
| Carbon steel | Below HRC30 | 80–120 m/min |
| Alloy steel | HRC30–40 | 60–90 m/min |
| Tool or mold steel | HRC40–50 | 45–70 m/min |
| Hardened mold steel | HRC50–55 | 30–50 m/min |
| Gray cast iron | Below HRC32 | 55–90 m/min |
| High-alloy cast iron | HRC35–45 | 40–65 m/min |
Reference Machining Parameters
| Cutter Dia. | Spindle Speed | Feed Rate |
|---|---|---|
| 4 mm | 4,000–6,000 rpm | 280–550 mm/min |
| 6 mm | 3,000–4,500 rpm | 320–650 mm/min |
| 8 mm | 2,200–3,500 rpm | 350–700 mm/min |
| 10 mm | 1,800–2,800 rpm | 350–720 mm/min |
| 12 mm | 1,500–2,300 rpm | 350–720 mm/min |
| 16 mm | 1,100–1,700 rpm | 320–650 mm/min |
| 20 mm | 850–1,400 rpm | 280–580 mm/min |
Customization & OEM Service
Custom cutting diameters, flute lengths, overall lengths, shank diameters, tool geometry, coatings, laser marking and private-label packaging are available according to your machining requirements.
Get a Quote for Your Cutting Tools
Contact PENGFU TOOLS for product selection, machining recommendations, customized solutions and a competitive quotation.